
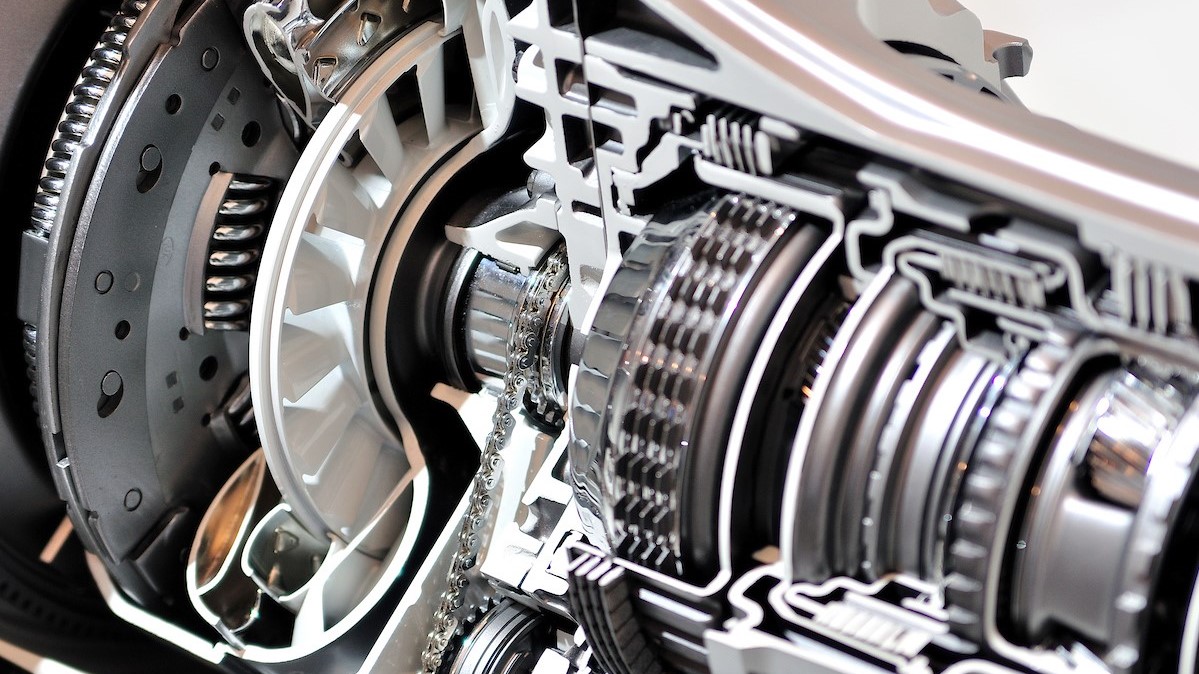
Anytime a rotating assembly is submerged in an oil bath, air bubbles, aka foam, can form on the fluid surface. Lubricants must be formulated to control foam to reduce the risk of mechanical damage.
For example, the crankshaft in engines can create foam in motor oil and differentials can create foam in gear oil. In motorcycles, shared-sump transmissions, where the transmission and engine use the same oil, are good at creating foam.
Foam in hydraulic lifters can create valvetrain noise because the foam is made of air that compresses and creates lash in the valvetrain.
Foam can lead to poor component protection and ultimately mechanical damage. That’s why controlling foam is a critical piece of lubricant formulation.

A Host of Issues
There are several ways that foam causes problems:
- Heat — Foam heats to extreme temperatures under pressure, generating steam within the fluid. Then, foam compounds the issue by creating an insulating layer that prevents the heat from dissipating. Heat and water contamination limit the lubricant’s effectiveness.
- Wear — Because air is trapped inside the fluid, the fluid barrier is no longer impenetrable and wear-causing metal-to-metal contact can occur.
- Oxidation — The air trapped in foam promotes oxidation and shortens the service life of the fluid.
Hydraulic and other industrial applications face another issue. When hydraulic fluids foam, they become compressible and can make machinery inoperable or extremely inefficient. These heavy-duty lubricants require special formulations to prevent foaming.
Friend or Foam
Controlling foam is not an easy task. Oil viscosity, contaminants, changes in surface tension and additives can all act as catalysts to the formation of foam.
Detergents and dispersants promote foaming and minimize the effectiveness of anti-foaming additives.
Anti-foam agents can stop foaming but require effective formulation to avoid trapping tiny bubbles within the lubricant.
Silicone additives are an example of how critical it is to get the formulation exactly right. Silicone compounds are widely used for their ability to reduce the surface tension of air bubbles. Reducing the surface tension causes the bubbles to break apart quickly and easily.
Silicone compounds in formulations of only a few parts per million can be extremely effective, however excess amounts can promote foaming.
Organic compounds can also decrease the number of small bubbles but require much higher concentrations than silicone.

Foaming Characteristics Test (ASTM D892)
A lubricant’s ability to resist foaming is measured with the Foaming Characteristics Test (ASTM D892). It measures the amount of initial foaming (in millimeters) contained within an agitated fluid and compares that value to the amount remaining after 10 minutes of settling time. Generally, the less foam remaining after a short amount of time, the better.
Built-In Resistance
AMSOIL synthetic oils are precisely formulated with anti-foam additives to resist the oxidation and acid formation that contribute to foam development. The suppression of foam improves mechanical performance and provides more reliable protection for your machines.
Video transcript: Tour the AMSOIL Mechanical Lab
I’m Mark Nahum, Staff Engineer and Mechanical R&D Manager for AMSOIL, and this is our mech lab. Let’s give you a little sneak peek of what this mechanical lab does for AMSOIL. It is a piece of our validation process for all of the products that we come to market. If I was just a blending facility, I wouldn’t need a mechanical lab to validate my products.
I take fully formulated versions from chemistry partners, I mix them together, and I sell them to consumers. But that’s not what we do here. We take it from the chemical level, we break it down, we make really good formulas, and then we need a place to validate them. Then, we take it down here in the mechanical lab and put those formulas to work in actual applications, whether it’s engines, transmissions, hydrostats, compressors.
That’s what we do here. There’s a difference between those that just blend and those that fully engineer their products. Every project that we work on here in the mechanic lab typically starts with an application out in the market. There’s a problem that we identify, or some customer has a need that is not currently being met by another lubricant.
We start with product requirements. We need a way to gauge success, so we bookend what this product should look like in the end. Then we go to work in our chemical lab. We start mixing formulations together and we use industry standard tests to get us successful on the bench level, but we don’t stop there.
We need to validate that product before we commercialize it. That’s why a mechanical lab is a huge asset to AMSOIL. We put those formulations into real engines. We beat them up, we put them through really long tests, insane temperatures, really heavy loads, all so that we can take all that data and see whether we’ve achieved success.
Now that you have a firm grasp of our validation process here in the mechanical lab, let’s go take a look at the capabilities of each of our cells. Our mechanical lab has three dyno cells. In cell 1, we have a SuperFlow water brake, where we’ll put anything from a small snowmobile engine, all the way up to 1,000 horsepower Hellephant engine. Dyno cell 2, a little more flexibility here, where we’ll run small engines on fixed test stands for hundreds of hours.
We’ll run weed whips and blowers, making noise for hundreds of hours. We have a Midwest eddy current, which is super accurate for long periods of time, where we’ll run small V6 or V8 engines, or we’ll adapt a different tester and run hydrostats from zero-turn lawn mowers. In our last cell, dyno cell 3, we have our SuperFlow roller dyno, where we’ll put motorcycles, dirt bikes, street bikes, side by sides, and we’ll take field data that we collect from the road in the woods doing hill climbs, and we’ll duplicate it on the dyno. Then, we’ll turn up the knob a little bit to reach what we consider sphere testing.
Very rarely do we make decisions around here based on subjectivity. We are in the business of measuring things. That’s how we learn, that’s how we formulate, that’s how we engineer, and that’s how we make products for you to sell to your customers. How do we measure stuff?
We use the tools built into our dynos, which is measuring horsepower, and RPM, and temperatures. We use data acquisition systems to measure a lot of some of those same things if they’re not really integrated to my dyno. Then, what we do is we graphically look at them, and we make sure that if we’re measuring power, or torque, or RPM, when we set up a dyno profile, we want to make sure that that engine is operating that profile every single time and its not deviating. If it’s a deviation from that, then something’s happening in the engine that we need to know about.
We take these measurements to make sure that our test is valid. At the end of this analysis, we shut down the engine or whatever might be on test of time, and then we tear it apart. That’s where the true physical measurements come in. We use measuring tools, and what we’re doing is we’re comparing before to after.
Let’s dive a little deeper into some of the documentation techniques we use in the mechanical lab. We use a high precision camera to document the before and after condition of the parts under test. What we’re looking for is deposits and wear. In this area of the mechanical lab is where we tear everything down.
This is where we physically measure the before and the after condition of everything that we’ve just taken off of test. For example, we have a Twister blower here, and we’re going to measure the difference between the wear that you might find in the cylinder. We’re going to measure the wrist pin. You look at a hydrostat transmission from a zero-turn lawn mower, we’re going to look at the pistons, and the swashplate that builds pressure and propels that thing forward.
We’re going to look at the deposits that form inside that case. You look at this set of cylinders from a snow machine. We’re going to pay particular attention to the bores, the cylinders, and we’re going to measure that profile difference from before and after. You look at a set of bearings on the other side of the table from the crank and the rods.
We want a before and after measurement of the wear to those bearings. The measurements that we take here are of the utmost importance to AMSOIL. We use these measurements to make decisions on new products coming to the market or new technologies that we’re investigating to put into the current products that we have on the market today. We put a lot of importance on this to help you be successful.
Hopefully, you can make it up here someday and see it yourself. But until then, we got to get back to work to work on the top secret projects that I can’t share with you. Thanks for coming. [ MUSIC ]
Comments
Brad Nelson is an AMSOIL Technical Writer II who develops content about lubricant technology, product performance and vehicle maintenance. He works with engineers and product specialists to translate testing, application requirements and approved performance claims into clear customer guidance. Nelson’s work includes AMSOIL Blog articles, AMSOIL Magazine features and technical explanations concerning motor oils, gear lubricants, vehicle systems and maintenance practices.
Share: